Corrosion-resistant and high-strength — places higher demands on cutting parameters and tooling.
1.4301 / X5CrNi18-10
1.4404 / X2CrNiMo17-12-2
Approved
Properties
Density
7.9 g/cm³
Austenitic chromium-nickel steel
Tensile strength
520–720 MPa
1.4301, depending on condition
Thermal conductivity
Low
Approx. 15 W/(m·K), heat accumulation at the cutting edge
Corrosion resistance
Very high
Resistant to many media, suitable for food and pharmaceutical applications
Machinability
Moderate
Prone to work hardening, requires sharp cutting edges
Machining
Challenge and solution
Challenge
Surface work hardening
Insufficient feed rates or interruptions in the cut harden the surface and complicate subsequent machining.
Our Solution
Defined, stable feed rate
A consistent, sufficiently high feed rate prevents hardening of the surface layer.
Challenge
Tool wear due to material toughness
The toughness of austenitic steels places higher stress on cutting edges than unalloyed steels.
Our Solution
Adapted cutting edge geometry
Sharp, positive geometries and suitable coatings reduce wear and heat input.
Challenge
Built-up edge at low cutting speeds
At excessively low cutting speeds, stainless steel tends to adhere to the cutting edge.
Our Solution
Optimized cutting parameters
Cutting speed and coolant supply are calibrated to prevent material buildup on the cutting edge.
Challenge
Dimensional accuracy during long machining times
Higher cutting forces and thermal input can lead to dimensional deviations during lengthy machining operations.
Our Solution
In-process measurement
Critical dimensions are inspected while clamped in the fixture and adjusted as needed.
Machining
How we machine this material
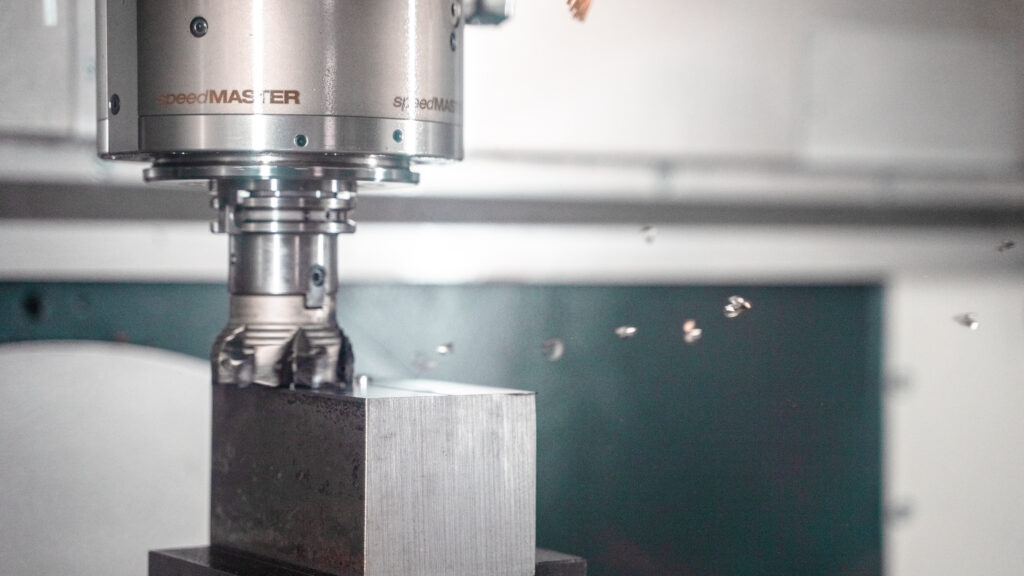
We machine stainless steel using sharp, positive-rake cutting edges and stable feed rates to prevent surface work hardening. Continuous cutting instead of interrupted cuts and sufficient flood cooling protect both the tool and the workpiece surface.
For us, quality is not just a word, but measurable reality. Through state-of-the-art testing equipment such as laser interferometers and 3D measurement technology, we ensure that every component precisely meets specifications.